The Roxas Necklace: A Technical Guide to Materials & Chain Gauges
An expert technical breakdown of the Roxas necklace, analyzing chain gauges, pendant metallurgy, and casting methods for premium replicas.
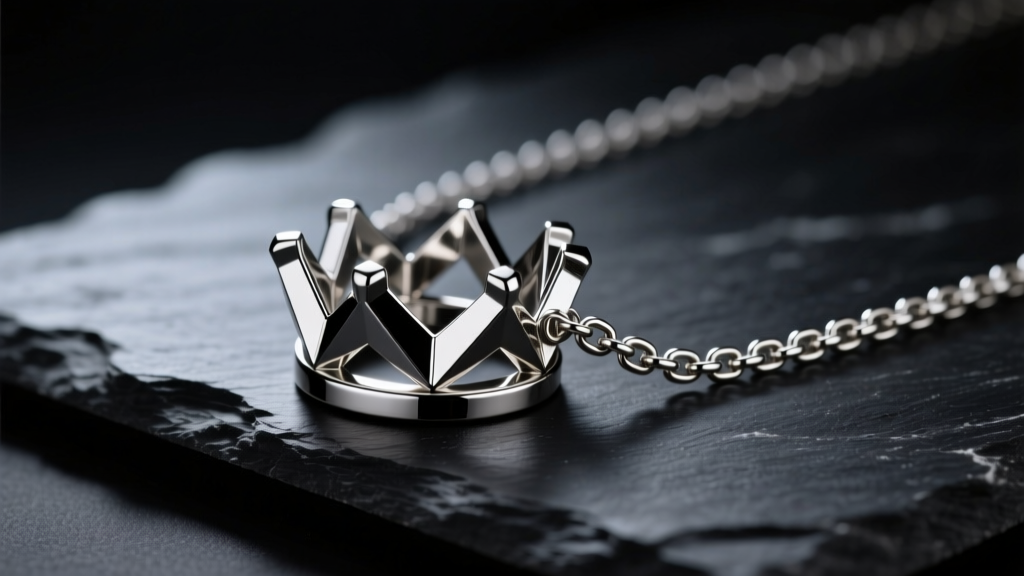
Architectural Blueprint of the Roxas Necklace
The Roxas necklace has transcended its origins in video game cosplay to become a staple in avant-garde streetwear and alternative fashion. Characterized by its heavy, oversized geometric crown and inverted emblem motif, the piece demands a robust structural foundation. However, the market is saturated with substandard replicas that fail under their own weight. As of 2026, discerning collectors and fabricators are moving away from cheap die-cast novelties, demanding precise metallurgical integrity and exact chain gauges. This deep dive explores the technical specifications required to engineer a premium Roxas necklace, focusing on material science, link topography, and advanced casting parameters.
Metallurgical Analysis: Base Alloys vs. Premium Alloys
The pendant of a Roxas necklace typically measures between 45mm and 60mm in height, resulting in a significant mass. Mass-market manufacturers default to Zamak (a zinc alloy containing roughly 5% aluminum and trace amounts of copper and magnesium). While Zamak offers a low melting point of approximately 385°C (725°F) and excellent fluidity for complex molds, it suffers from severe long-term degradation. Zamak is highly susceptible to intergranular corrosion and "tin pest" if exposed to high humidity, leading to surface blistering and structural brittleness over time.
For a heritage-grade replica, fabricators must utilize either 316L surgical stainless steel or .925 sterling silver. 316L steel contains 16-18% chromium, 10-14% nickel, and 2-3% molybdenum. The "L" denotes low carbon, which prevents carbide precipitation during high-heat polishing, ensuring the alloy maintains a Vickers hardness (HV) of 150-190. This hardness is critical for resisting the micro-abrasions that occur when a heavy pendant strikes the wearer's sternum. According to the Gemological Institute of America (GIA), while .925 sterling silver offers superior acoustic resonance and a traditional luxury feel, it requires a rhodium flash or strict anti-tarnish storage to prevent sulfur-induced oxidation.
| Alloy | Density (g/cm³) | Vickers Hardness (HV) | Corrosion Resistance | Estimated Cost per Gram |
|---|---|---|---|---|
| Zamak 5 (Zinc Alloy) | 6.7 | 80 - 100 | Poor (Prone to blistering) | $0.01 - $0.03 |
| 316L Stainless Steel | 8.0 | 150 - 190 | Excellent (Marine grade) | $0.05 - $0.08 |
| .925 Sterling Silver | 10.3 | 60 - 80 (Annealed) | Moderate (Tarnishes) | $0.70 - $1.20 |
Chain Topography: Curb vs. Rolo Link Extrusion
The chain is not merely a suspension system; it is a foundational design element of the Roxas aesthetic. The original design language calls for a heavy, interlocking chain that lays flat against the clavicle. This necessitates a curb chain profile rather than a standard rolo or cable chain. A true premium replica utilizes a 10mm to 12mm curb chain with a minimum wire thickness of 2.5mm (approximately 10 AWG).
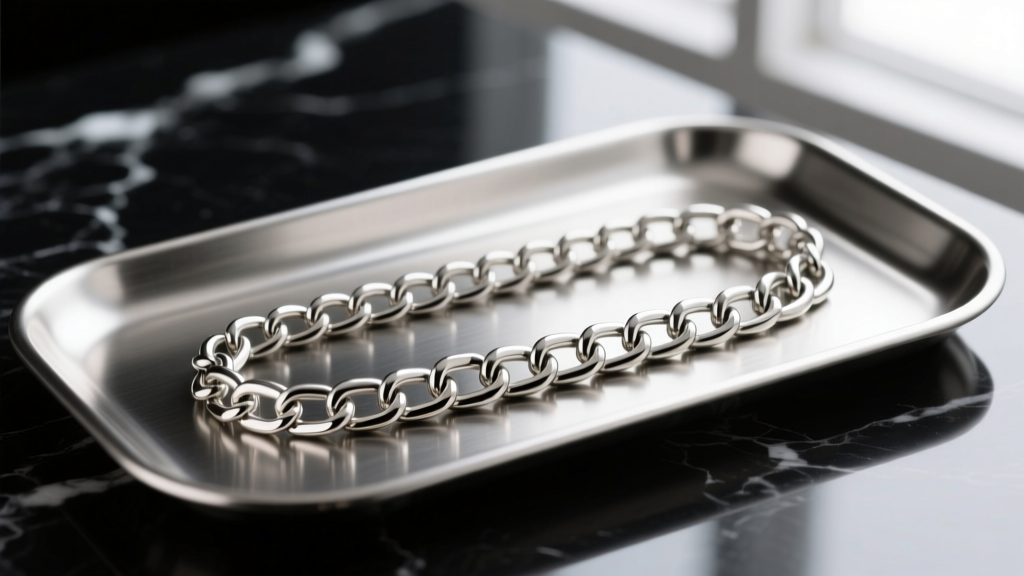
The Hollow-Link Deception
Many mid-tier replicas utilize hollow-extruded links to mimic the visual bulk of a 12mm chain while keeping the weight and material costs down. Hollow links are manufactured by wrapping thin metal sheeting around a resin core or using electroforming techniques. Under tensile stress—such as the pendant catching on a garment—hollow links will crush and deform irreparably. Solid-link extrusion, where a solid wire is fed through a CNC chain-making machine and diamond-cut for faceting, ensures a tensile strength exceeding 40 kg (88 lbs), which is mandatory for supporting a 100g+ pendant without catastrophic failure.
Pendant Fabrication: Investment Casting Parameters
To achieve the sharp, aggressive angles of the geometric crown and inverted emblem motif, lost-wax investment casting is the only viable fabrication method for precious metals. As of 2026, master patterns are predominantly CNC-milled from high-density jeweler's wax or 3D printed using castable photopolymer resins with an ash content of less than 0.05%.
The burnout cycle is the most critical phase. The investment flask must be heated to 730°C (1350°F) for a minimum of 8 hours to completely vaporize the wax residue. Any residual carbon will cause surface pitting and porosity in the final cast. Jewelry fabrication suppliers like Rio Grande emphasize that when casting heavy, thick pieces like the Roxas pendant, the flask must be centrifuged at a minimum of 300 RPM, or cast in a vacuum environment, to force the molten metal into the deepest recesses of the geometric grooves before the metal begins to freeze.
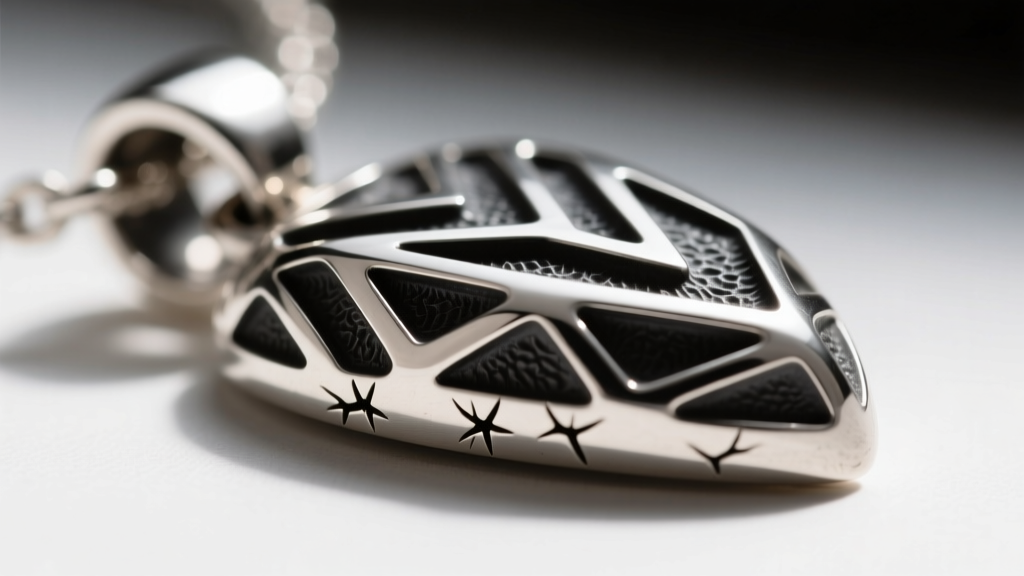
Surface Finishing: Liver of Sulfur and Brushed Textures
A raw cast pendant lacks the visual contrast required for the Roxas design. The interplay between light and shadow is achieved through selective oxidation. The piece is submerged in a warm solution of liver of sulfur (potassium polysulfide) diluted in distilled water. This chemical reaction rapidly accelerates the formation of silver sulfide, turning the entire piece black.
Following oxidation, the pendant is mounted on a magnetic tumbler or polished using a radial bristle wheel. The goal is to remove the black patina from the high-polish, raised edges while leaving the dark oxidation trapped in the recessed geometric lines. For stainless steel variants, a similar contrast is achieved by media-blasting the recesses with glass beads to create a matte, light-diffusing texture, while the raised edges are mirror-polished using a rouge compound.
Clasp Mechanics and Tensile Load Limits
The failure point of 80% of heavy chain necklaces is the clasp assembly. A standard 12mm lobster clasp, typically rated for a maximum working load of 5 kg, is entirely insufficient for a heavy curb chain and solid pendant. The dynamic force generated when the wearer moves can easily exceed the tensile limit of a standard clasp's internal spring mechanism.
Expert fabricators utilize a heavy-duty T-bar toggle clasp or a 25mm reinforced trigger clasp machined from the same 316L steel as the chain. If a toggle is used, the T-bar must be at least 18mm in length to prevent it from slipping through the receiving ring during lateral movement. Furthermore, the jump rings connecting the clasp to the chain must be soldered closed or utilize a split-ring mechanism with a wire gauge no thinner than 14 AWG (1.6mm).
Ergonomics and Cervical Weight Distribution
A fully fabricated, solid-link Roxas necklace can easily weigh between 150 and 250 grams. Concentrating this mass at the base of the throat causes cervical strain and discomfort. To mitigate this, the chain length must be carefully calibrated. A 20-inch to 22-inch drop allows the pendant to rest on the sternum, distributing the weight across the broader musculature of the upper chest rather than the delicate cervical spine. Additionally, flattening the back of the pendant bail (the loop connecting the chain to the pendant) prevents the pendant from flipping backward and choking the wearer during active movement.
Sourcing and Authenticity Verification
When evaluating a premium Roxas necklace, inspect the interior of the chain links and the back of the pendant bail. Authentic solid links will show a continuous grain structure without visible seams, while high-quality cast pendants will bear a subtle stamp indicating the metal purity (e.g., "925" or "316L") and the fabricator's hallmark. Avoid pieces that exhibit a grayish, dull sheen on the high-polish edges, as this is a telltale sign of zinc alloy attempting to mimic the luster of rhodium-plated silver or polished steel through cheap electroplating processes.